
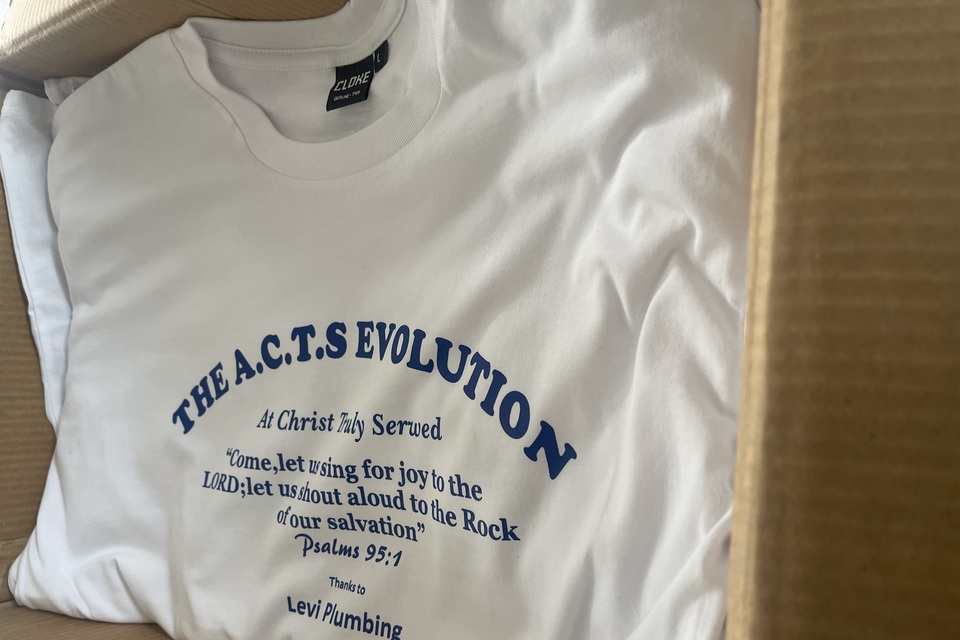
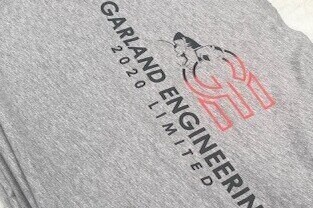
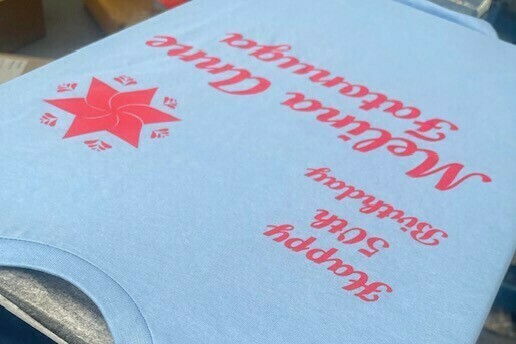
If you’re looking for a high-quality print that will hold up wash after wash, then screen printing is the choice for you.

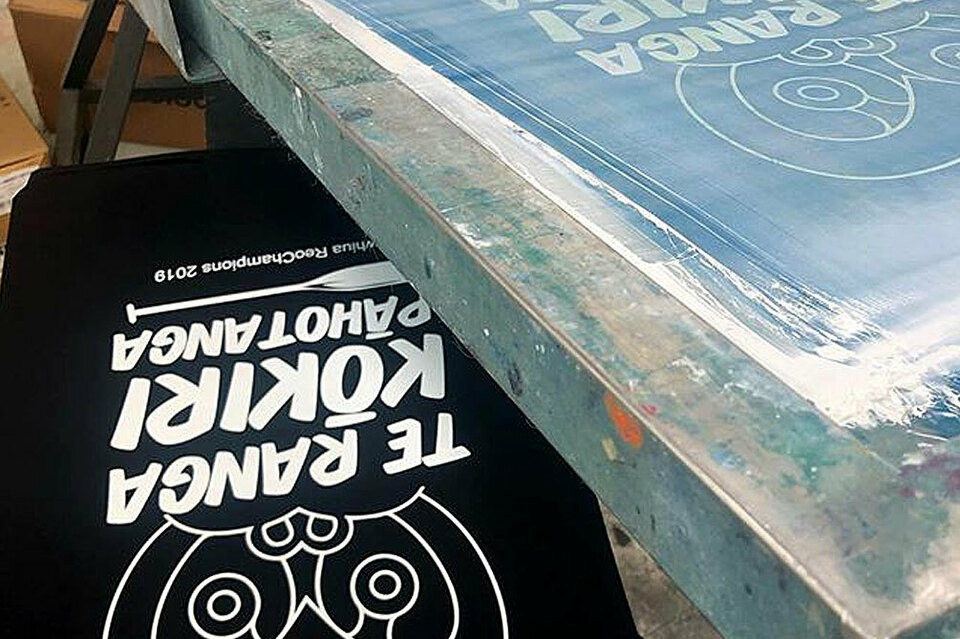
Today screen printing is a popular and cost-effective option for creating bold, durable, and vibrant prints, especially for large quantities of items like t-shirts, hoodies, shirts, tea towels, tote bags and more. The process involves creating a stencil on a screen, placing it over the apparel, and using a squeegee to force ink through the stencil, transferring the design onto the fabric.
PUFF SCREEN PRINTING
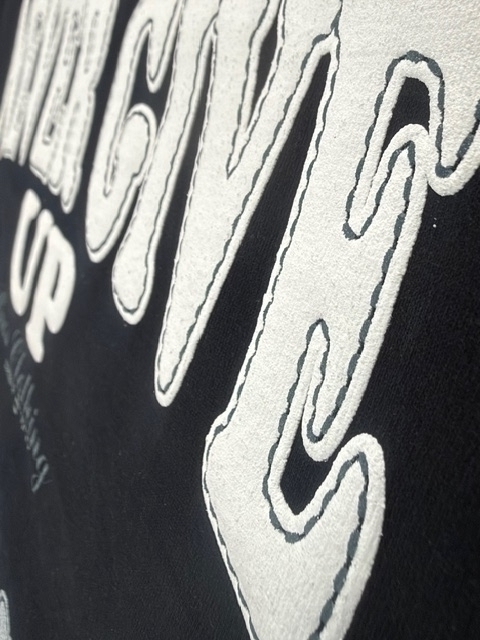
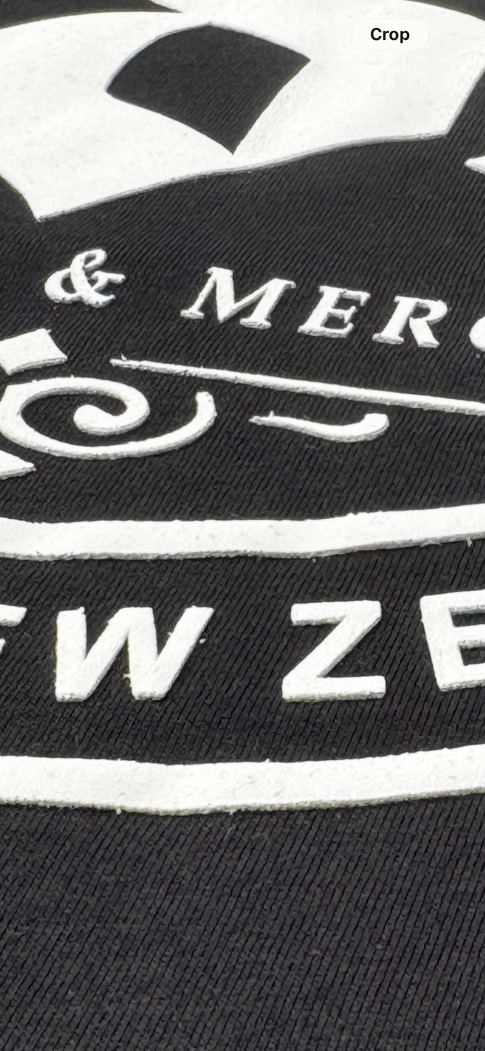
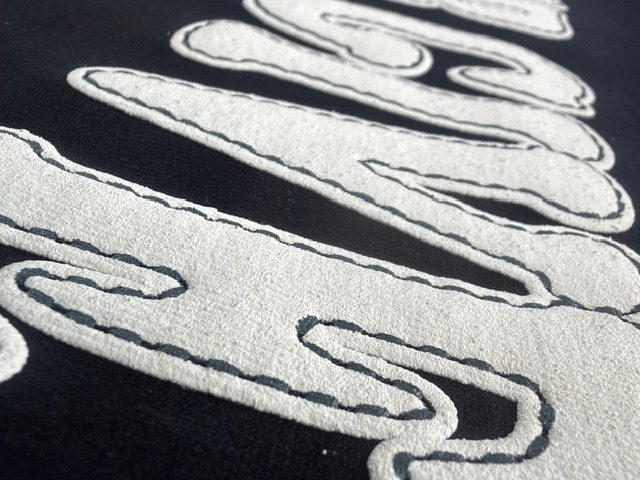
Puff Screen Printing: Uses a special heat-expanding additive mixed into the plastisol ink. When cured under heat, the ink bubbles and rises off the fabric to create a raised, 3D, tactile finish.
HIGH DENSITY SCREEN PRINTING
HD (High-Density) Screen Printing: Uses a thick emulsion stencil (often with high-density clear base or thick ink layers) to lay down a heavy, raised deposit of ink with sharp, defined edges
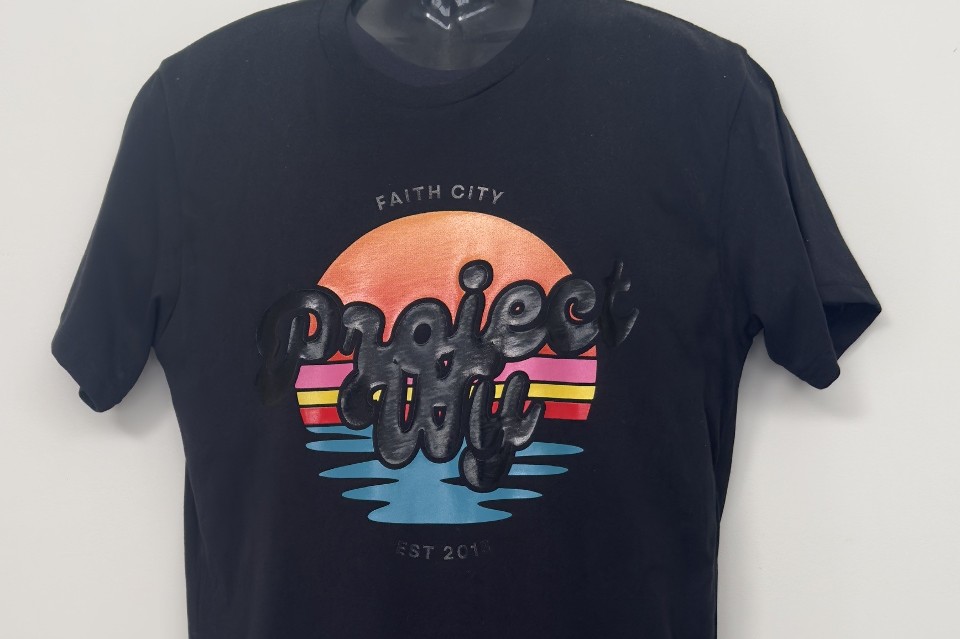
CMYK (Four-Colour Process):
Prints tiny halftone dots of Cyan, Magenta, Yellow, and Black to create full-spectrum and photographic images. Works best on white or light-coloured fabrics
The six main screen printing techniques are spot color, halftone, grayscale, duotone, CMYK (four-color process), and simulated process.
- Spot color: Uses solid, opaque inks—one screen per color—for bold graphics and 1–4 color designs on light or dark fabrics.
- Halftone: Creates shading and gradients using a single ink color broken into small dots of varying sizes.
- Grayscale: Renders full-color or photographic images using a single ink color (often black or white) in halftone dot patterns.
- Duotone: Combines two halftone screens—typically black plus one accent or spot color—for a two-tone or retro look.
- CMYK (four-color process): Layers transparent cyan, magenta, yellow, and black halftone inks to reproduce full-color photos and gradients, typically on light-colored surfaces.
- Simulated process: Blends halftone screens with opaque spot inks to achieve rich, photographic detail on dark garments without needing a white base across the whole print
How it Works (Simplified)Create the Screen:
A design's negative (where ink shouldn't go) is applied to a mesh screen stretched on a frame, blocking those areas with a stencil (often using photo emulsion). Prepare for Print: The screen is placed over the item (like a t-shirt) on a printing press. Apply Ink: A squeegee spreads ink across the screen; it goes through the open mesh onto the item. Cure: The ink is then dried and "cured" with heat (like a conveyor dryer or heat gun) to set it permanently. Multi-Color: Each color requires a separate screen and print pass, carefully aligned (registered).
Key Garment Types & Fabrics for Screen Printing:
T-shirts & Tanks: The most popular choice for bulk promotional gear, band merchandise, and custom apparel.(100% cotton)Workwear (Polos & Hi-Vis): Suitable for durable branding on materials like cotton blends. Hoodies & Sweatshirts: Ideal for heavy-duty prints, specifically cotton blends. Woven & Casual Wear: Includes denim, trackpants, and other flat or slightly textured materials.
HD SCREEN PRINT
PUFF SCREEN PRINTING
SCREEN PRINTING
Product Title
PUFF SCREEN PRINTING
CYMK SCREEN PRINT
SCREEN PRINTING


Contact us to discuss quotes and the details of our service.